A cracked casting looks fine from across the room. So does a bracket with a hairline burr, or a circuit board with one solder joint that didn’t quite take. Problems like these hide in plain sight, and for most of manufacturing history the only defence was a trained person looking closely, part after part, shift after shift.
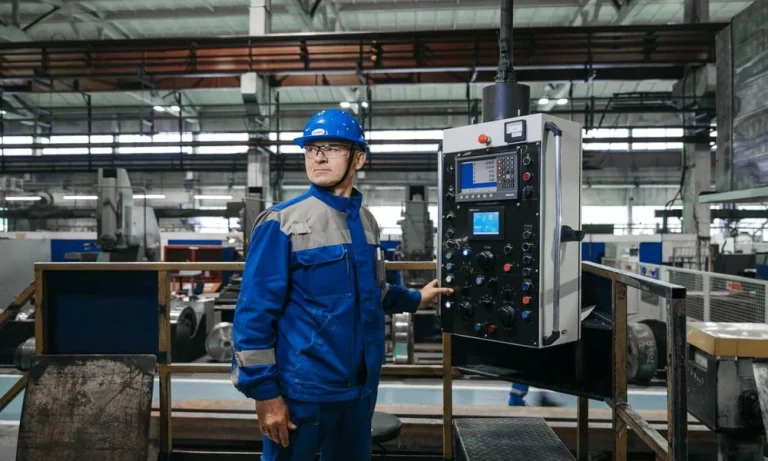
Industrial vision systems are taking over a good share of that work. Pair a well-lit camera with a model trained on real production images and you get an inspector that doesn’t drift, doesn’t rush before lunch, and keeps a record of every single decision it makes. Here’s how that plays out on an actual factory floor, and what separates the projects that pay off from the ones that quietly stall.
Why Human Inspection Hits a Ceiling
People are good at judgement and poor at repetition. Studies of visual inspection work have long shown that accuracy drops as a task grows monotonous, and anyone who has stood at a line for a full shift knows why. The defect rate you can catch at 8 a.m. isn’t the rate you can catch at 3 p.m.
Speed is the other limit. Modern lines can run faster than the eye can follow, particularly in packaging, electronics, and small-part assembly. A camera capturing an image in a fraction of a millisecond doesn’t need the line to slow down, and it can examine every unit rather than a sampled few. That shift from sampling to checking everything is, in many plants, the single biggest change in how quality gets managed.
What Sits Inside a Working System
It helps to think of a vision system as a chain with four links: lighting, optics, processing, and decision logic. Weakness in any one of them limits the rest. A superb algorithm fed dim, uneven images will still perform badly, which is why experienced integrators often spend more design time on lighting angles and lens selection than on software.
This is also where specialist knowledge earns its keep. Firms such as Industrial Vision Systems design the whole chain together, matching camera, lighting, and trained model to the specific part and line speed rather than dropping generic hardware onto a conveyor and hoping for the best. That joined-up approach matters most on awkward products: shiny metal, transparent plastic, textured surfaces, anything that bounces light in unhelpful directions.
Castings, Circuit Boards, and Other Tricky Jobs
Take metal casting, a process we’ve looked at on this blog in our piece on why casting remains the engine of modern manufacturing. Castings are wonderful for complex shapes, but they come with their own defect family: porosity, shrinkage cavities, surface cracks, incomplete fills. Some show up on the surface and suit camera-based checks. Others sit inside the part, where X-ray imaging combined with the same pattern-recognition techniques does the job. Either way, automated analysis gives a foundry a consistent pass or fail standard across thousands of parts.
Electronics assembly offers another clear example. Boards carry hundreds of tiny joints and components, and the industry developed dedicated camera-based checks long ago. If you want the background on how that field works, the Wikipedia entry on automated optical inspection gives a good overview of how cameras scan boards for missing parts, misalignment, and solder faults. Today’s AI-driven systems build on that foundation, handling variation that older, rule-based tools struggled with.
Why Some Projects Disappoint
The technology rarely fails outright. It disappoints because of how it’s introduced. The usual culprits are painfully ordinary. Too few defect examples to train on, so the model has barely seen what a bad part looks like. Lighting that changes with the time of day. A product revision nobody told the vision team about. Or a rejection rate so jumpy that operators lose faith and start overriding the system.
Good teams plan around these from day one. They gather images across several shifts and material batches, they agree with production staff what counts as a genuine defect, and they set up a simple way for operators to challenge a decision so the model can learn from the correction. Trust is a design requirement, not a nice extra.
Measuring the Payoff
Direct savings are the easy part to count: scrap, rework, returns, and inspection hours. The less obvious gains tend to arrive later. Because every inspection leaves behind an image and a timestamp, quality engineers can trace a problem to a particular tool, batch, or shift instead of quarantining a week’s output. Patterns also emerge, such as a die slowly wearing or a supplier’s material subtly changing, long before they’d show up in customer complaints.
For regulated products, that traceability can matter as much as the defect catch itself, because it lets a manufacturer show exactly what was checked, when, and against which standard.
Where to Begin
Start narrow. Pick one inspection point where defects are costly and clearly defined, run the system alongside your existing process for a few weeks, and compare results before relying on it. Ask early who will maintain the model, how new product variants get added, and what happens when the system is unsure.
Do that, and a vision system stops being a gadget and becomes an ordinary, dependable part of how your plant keeps quality steady, which is exactly the job it was meant to do.